Hey folks, if you’re deep in the plastic mould game—whether you’re a product designer, a production manager, or just someone trying to nail down cost projections for a new part—you’ve probably heard the term “cycle time” thrown around a lot. As a plastic mould supplier who’s been in this space for over a decade, I can tell you this: cycle time isn’t just some industry buzzword. It’s the single biggest factor that decides how fast you turn parts around, how much you pay per unit, and how reliable your production schedule is. Mess it up, and you’re looking at thousands in wasted material, idle equipment, and missed delivery deadlines that can tank a client’s trust. Mess it right, and you’re cranking out quality parts faster, for less, and keeping your line running smoothly. Let’s break this down like I’d explain it to a new shop floor trainee, no fancy jargon needed. Plastic Mould

First off, let’s define what a plastic mould’s cycle time actually is. Put simply, it’s the total length of time from when a mould closes, injects molten plastic, cools solid, and opens back up to eject the finished part. Think of it as one full “lap” around the mould machine’s routine. A lot of people new to this only count the injection part, but that’s a huge mistake—cooling makes up 70-80% of the cycle, that’s where most of the time hides. Skip that part, and you’ll get a part that bends in the box or cracks five minutes after it leaves the plant. The ideal cycle time depends on the part’s size, material, complexity, and the mould’s design, but typical numbers range from 15 seconds for tiny, simple parts (like a bottle cap) to 5 minutes or more for big, thick parts (like a car bumper). If your cycle time’s dragging, every minute you’re not ejecting parts is money you’re leaving on the table. For example, if you run a 100-ton injection mould machine that costs $150 an hour to operate, cutting a 2-minute cycle down to 1 minute shaves 150 parts per hour off the line, which adds up to 1,200 extra parts per shift—no new equipment required. That’s the kind of number that makes shop managers do a double-take.
Now, let’s talk about the biggest mistakes I see shops make when they’re trying to optimize cycle time. First, they rush cooling. Yeah, cranking up the coolant flow or turning down the water temperature sounds easy, but push it too far, and you’ll get thermal shock—cracks in the mould walls, warped parts, even mould failure that takes days to fix. I had a client once who tried cooling a polypropylene spool with 10°C water instead of 20°C, thinking it would cut 10 seconds off the cycle. Within a week, half his mould cavities had micro-cracks, and he was throwing away 30% of his parts for defects. That 10-second gain cost him $20k in repairs and delayed his delivery by two weeks. Second mistake: underengineering the mould for the part. A lot of people use a standard 2-cavity mould for a part that could easily handle 4 or 6 cavities, but they’re scared of the upfront cost. Sure, a multi-cavity mould might cost 30% more, but if you’re doubling your output per cycle, you’ll pay that back in three months, not years. Third, ignoring secondary operations. If your part needs to have a hole drilled or a label applied after ejection, that’s extra time you’re not accounting for. A part that looks simple might need 10 seconds of post-processing, which turns a 1-minute cycle into 1 minute 10 seconds—no big deal, but those seconds add up.
Okay, so how do you actually optimize cycle time without breaking the mould or ruining part quality? Let’s get into the actionable stuff, stuff we actually test in our shop every day:
First, nail the cooling system design. Like I said, cooling is the big one. The best moulds have conformal cooling lines—lines that follow the exact shape of the part inside the mould, instead of the old straight, boring lines that just run parallel. Conformal cooling cuts cooling time by 20-40% because heat doesn’t have to travel as far to escape from the plastic. For a thin part (1-2mm), a straight line might work, but for a 5mm thick part, conformal cooling is non-negotiable. We use 3D printed mould inserts for some of our more complex parts, because it lets us make those conformal lines that would be impossible to machine with traditional methods. Another trick: temperature control. Match the coolant temp to the material, not the machine. For most common plastics (PP, PE, ABS), a 18-22°C coolant temp is perfect—it cools fast enough without causing thermal stress. If you’re running a high-performance material like nylon or polycarbonate, bump it up a bit to avoid warping. Also, use insulated mould plates around the cooling lines—traps the heat inside the mould, so the coolant doesn’t have to work as hard, which saves time and energy.
Second, streamline the mould’s actuation and ejection. The part where the mould opens and closes, and pushes the part out—small delays here add up. A lot of older moulds use hydraulic actuators that take a second to switch speed, but we use electric servos now for new builds. They’re faster, more precise, and don’t waste energy idling. For ejection, use ejector pins that are sized right for the part—too small, and they’ll bend; too big, and they leave marks. We also add ejection timing adjustments: don’t eject the part the second the mould opens, wait half a second so the plastic has time to relax a little, that cuts down on part breakage. One client was having 15% of parts break during ejection, so we adjusted the pin placement and timing, and that dropped to less than 1%—no cycle time loss, just smarter setup.
Third, use the right material and screw design for the machine. The material you inject matters a lot. Some plastics melt faster, flow easier, and solidify quicker than others. If you’re using a high-viscosity plastic, you might need to raise the injection pressure or speed, but too high and you’ll flash plastic between the mould halves, which means you have to stop and clean it every cycle. Match your injection screw to the plastic: for amorphous plastics like ABS, use a general-purpose screw; for crystalline plastics like PP, use a screw with a deeper channel to handle the melting. Our team tests every new mould’s screw and material setup before we ship it, so our clients don’t have to waste time tweaking it on their end.
Fourth, don’t overlook the hot runner system if you’re using one. A hot runner keeps the plastic molten between cycles, so you don’t have to re-melt new plastic every time the mould closes. That cuts down on injection time and reduces material waste. But if your hot runner is old, it might have cold spots where plastic solidifies, which means you have to purge the system every few cycles—wasting plastic and time. Upgrade to a balanced hot runner system, where every cavity gets the same amount of plastic at the same temp, and you can cut out purge time entirely. We’ve had clients switch from cold runner to balanced hot runner and cut cycle time by 25% almost overnight.
Now, let’s talk about when to push too far vs. when to stop. I know, everyone wants the fastest cycle possible, but there’s a point of diminishing returns. If you cut cooling time too much, you’ll get parts that are undercooked—they might look good when they come out, but they’ll shrink or warp when they’re exposed to room temperature or stress. We did a test a while back on a small plastic gear: a 1.5mm thick part. A 2-minute cycle gave a perfect gear, but a 1-minute cycle had parts that warped 0.5mm within 24 hours. So we settled on a 1:15 minute cycle, which gave zero defects and was 25% faster than the original setup. Another thing: your mould machine’s capacity. If you’re running a 150-ton machine for a part that only needs 50 tons, you can adjust the clamping speed and pressure to match, which cuts down on close/open time. A lot of shops run their machines at 100% capacity even when they don’t need it, which is like driving a truck to the grocery store—you’re using way more power than you need.
Also, regular maintenance is key to keeping cycle time consistent. A mould with worn ejector pins or dirty cooling lines will start to drag cycle time over time. We recommend cleaning moulds every 2-3 months, inspecting cooling lines for clogs, and replacing worn parts like seals and pins on a schedule. One of our long-term clients skipped a mould cleaning for 6 months, and their cycle time went from 1.2 minutes to 1.8 minutes—all because a cooling line was clogged with plastic residue. That’s a mistake that’s 100% avoidable.
Now, let’s tie this back to what it means for you, as someone who’s looking to work with a mould supplier. The right supplier won’t just give you a mould that works—they’ll design it for your specific cycle time needs, not a one-size-fits-all. A lot of cheap moulds cut corners on cooling, so you’ll be stuck with long cycles and high defect rates. We design every mould with your production volume and timeline in mind: if you need 1 million parts a year, we’ll make sure the cycle time is optimized for your machine, not some generic spec. We also provide post-installation support—if your cycle time starts dragging, we’ll help you troubleshoot whether it’s the mould, the machine, or the setup, no extra fees.
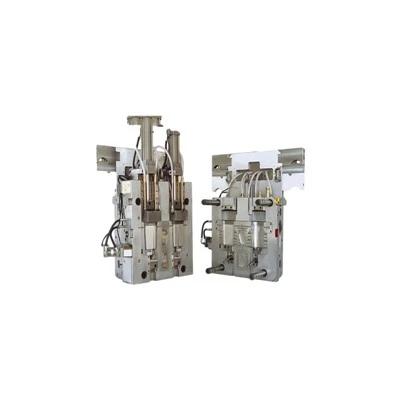
At the end of the day, cycle time optimization is all about balance. You want the fastest possible cycle without sacrificing part quality, mould lifespan, or your bottom line. It’s not about rushing parts; it’s about working smarter, not harder. If you’re tired of dealing with moulds that drag their feet, have too many defects, or leave you guessing, we’re here to help. We don’t do generic moulds—we build moulds that fit your production goals, so you can crank out quality parts on time, every time. If you’re ready to stop wasting time on inefficient cycles and start hitting your delivery targets, reach out to our team to chat through your project. We’ll walk you through every step, no sales jargon, just straight talk about how to make your plastic production run smoother.
Mould Components References:
- Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook (3rd ed.). Springer.
- Beamon, B. M. (1999). Design for injection molding: Reducing cycle time and improving part quality. Marcel Dekker Inc.
- Groover, M. P. (2020). Fundamentals of Modern Manufacturing: Materials, Processes, and Systems (7th ed.). John Wiley & Sons.
- International Molders and Association. (2021). Best Practices for Cycle Time Optimization in Injection Molding.
- Britton, G. A. (2018). Conformal cooling: A game-changer for injection mold cycle time reduction. Journal of Injection Molding Technology.
Wuxi Santaizi Metal Products Co., Ltd.
As one of the most professional plastic mould manufacturers and suppliers in China, we warmly welcome you to buy high-grade plastic mould made in China here from our factory. All customized metal products are with high quality and competitive price. Contact us for pricelist.
Address: No. 23 Xufeng Road, Xushe Town, Yixing City, Wuxi City, Jiangsu Province, China
E-mail: Ksstzmj@163.com
WebSite: https://www.wuxisantaizi.com/
